Radical Materials develops and manufactures metal detectable and X-ray detectable compounds and masterbatches for plastics, silicone and rubber in the UK, primarily for food and pharmaceutical processing applications. SCOPIC® materials are available in polymers including TPU, PA, POM, polyketone, PP and PE, as well as silicone and rubber.
Standard and custom formulations are supported by in-house metal detection and X-ray inspection equipment, allowing detectability, mechanical performance, processing and colour to be evaluated and optimised during development.
Employing SCOPIC metal detectable plastics & x-ray detectable plastics in place of standard polymers enables contaminants to be detected by conventional detection systems.
Foreign body contamination, such as metal, bone, glass and plastics, is a major area of concern for processors & manufacturers in the food and pharmaceutical industries. Should these foreign bodies pass into the consumer chain, they cause significant risk to consumers, as well as financial and reputational implications for the manufacturers. To mitigate this risk, production lines will commonly employ metal or x-ray detection systems at critical control points, however standard plastics & rubbers are generally undetectable.
Have a question? We are always happy to chat, so feel free to give us a call on +44(0)1495211400.
Replacing conventional plastics with detectable materials helps address the risk of polymer fragments entering the product stream, supporting effective hazard analysis and control measures within food production environments.
Metal and X-ray detectable polymers provide an additional layer of control by allowing fragments from damaged or worn components to be identified by appropriately configured inspection systems before contaminated product reaches the consumer.
Detectability can help identify foreign-body contamination during production, reducing the risk of affected products leaving the facility and the potentially significant costs associated with product withdrawal or recall.
Foreign-body incidents can damage consumer confidence and customer relationships as well as creating direct financial costs. Specifying detectable materials for appropriate components helps demonstrate a proactive approach to contamination risk and product safety.
SCOPIC® materials are developed around the complete requirements of the finished component. Detectability is optimised alongside mechanical performance, processing behaviour, colour and regulatory requirements rather than being treated as an isolated material property.
SCOPIC® formulations use carefully selected additive systems to achieve high levels of metal and/or X-ray detectability. Optimising the efficiency of the detectable system can allow the required performance to be achieved at lower additive loadings, helping to minimise unwanted effects on the base polymer.
Detectable additives can reduce toughness, impact strength and other mechanical properties if they are incorporated at excessive loading or without appropriate formulation.
SCOPIC® materials are developed to balance detectability with the performance requirements of the finished component. Where necessary, polymer-specific impact modification, flow promotion and other formulation techniques are used to help retain toughness and processability.
Detectable polymers are commonly specified in bright colours, particularly blue, to provide an additional level of visual identification in food-processing environments.
Many detectable fillers naturally produce dark or muted compounds. SCOPIC® formulations can be designed to achieve bright, clean colours, including unusually light and white engineering polymers, while retaining the required detection performance.
Many SCOPIC® materials are used in or around food-processing equipment, including components intended for direct or indirect food contact. Regulatory requirements are therefore considered during formulation, with appropriate declarations and supporting migration data available for relevant products and conditions of use.
Drawing on extensive in-house formulation and compounding expertise, SCOPIC® materials can be tailored to suit the polymer, manufacturing process and required level of detectability. Additive loading, carrier, colour and other properties can be adjusted to achieve the best balance of detection performance, processability and mechanical properties.
Not all metal and X-ray detectable materials are developed or manufactured by the company selling them. In many cases, detectable compounds are sourced from third-party manufacturers, limiting the supplier’s control over formulation, consistency, technical support and product development.
SCOPIC® materials are different. Radical Materials develops, compounds and manufactures detectable materials in-house, giving us direct control over the complete process from initial formulation through to testing and commercial production.
Detectability is only one part of material performance. Adding detectable fillers can affect impact strength, flexibility, wear resistance, processing behaviour, colour and surface finish.
Because we formulate and compound SCOPIC materials ourselves, we can balance detectability with the mechanical and processing requirements of the finished component, rather than relying on a fixed off-the-shelf formulation.
Applications vary considerably. The polymer, manufacturing process, component geometry, operating environment and detection equipment can all influence the optimum formulation.
SCOPIC materials can therefore be developed or modified rapidly in-house. Small-scale compounding, moulding or extrusion trials, detectability testing and mechanical evaluation can all be carried out before progressing to commercial manufacture.
Simply adding a detectable filler does not guarantee that a finished component will provide adequate detection performance.
We can manufacture representative test samples and assess them using industrial metal detection and X-ray equipment, allowing additive level, material composition and component design to be evaluated before production.
The same technical team responsible for developing SCOPIC formulations is involved in their manufacture. This provides greater continuity between laboratory development, production scale-up and ongoing supply, while reducing reliance on external manufacturers or unknown formulation changes.
When questions arise about processing, detectability or material performance, customers can speak directly to the people who develop and manufacture the material.
That means faster answers, faster problem solving and greater flexibility when an application requires something outside the standard SCOPIC range.
Metal and X-ray detectable plastics are widely used in food-processing equipment to reduce the risk of undetected polymer fragments entering the product stream.
Metal and X-ray detectable polymers are widely used for modular conveyor links, rods, guides and flexible belting. Engineering polymers such as POM, nylon and polyketone can be used for rigid components, while detectable TPU and PVC are suited to flexible belts and profiles.
Detectable cable ties and fasteners are widely used around food-processing equipment. If damaged, fragments can be identified by metal and/or X-ray inspection systems rather than remaining effectively invisible within the product stream.
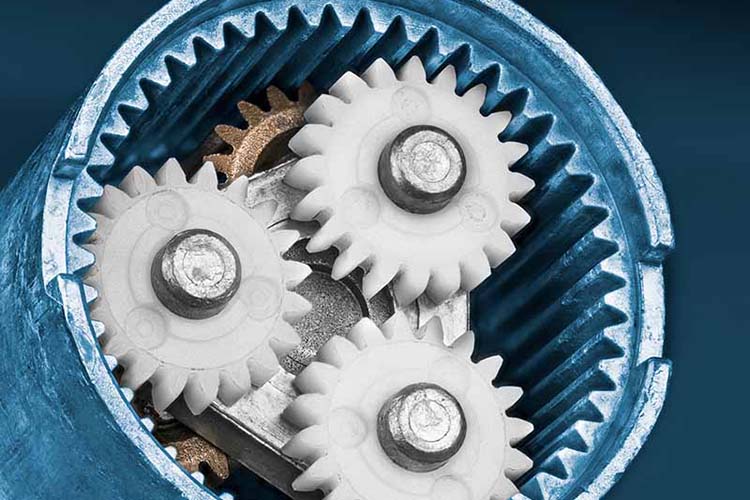
Guides, wear strips, gears, bushes and other polymer components may gradually wear during operation. Using detectable materials helps ensure that fragments generated through wear have a greater chance of being identified by appropriately configured inspection equipment.
Elastomeric seals and gaskets can be damaged or sheared during use or maintenance. Metal and X-ray detectable silicone and rubber provide an additional level of foreign-body control for these difficult-to-see components.
Scrapers, paddles, scoops, blades and other polymer tools may be exposed to repeated impact, abrasion and cleaning. Detectable materials provide an additional control measure where fragments could enter food during use.
Handles, covers, guards, knobs, rollers and other polymer components used around production lines can also be manufactured from detectable compounds, particularly where wear or accidental damage could create a foreign-body risk.
SCOPIC® metal and X-ray detectable technology can be incorporated into a wide range of thermoplastics, elastomers, silicones and rubbers. Formulations can be supplied as ready-to-process compounds or as masterbatches for incorporation into a customer’s existing polymer.
| Polymer | Typical attributes | Typical SCOPIC applications | Processing |
|---|---|---|---|
| TPU | Flexible, abrasion resistant | Belts, profiles, flexible parts | Extrusion / injection moulding |
| POM/Acetal | Low friction, dimensionally stable | Gears, wear components, guides | Injection moulding |
| PA/Nylon | Tough, strong | Engineering components, links | Injection moulding/extrusion |
| PK/POK | Tough, wear/chemical resistant, low moisture uptake | Conveyor and engineering components | Injection moulding |
| PP/PE | Chemical resistant, economical | General food-processing components | Injection moulding/extrusion |
| Silicone/rubber | Flexible/sealing properties | Seals, gaskets, bellows | Elastomer processing |
Detectable thermoplastic polyurethane (TPU) compounds are particularly suited to flexible components, conveyor belting, profiles and other applications requiring a combination of toughness, flexibility and abrasion resistance. We have extensive experience developing detectable TPU formulations while minimising the effect of detectable additives on mechanical and processing properties.
POM combines stiffness, dimensional stability, low friction and excellent wear characteristics, making it widely used for engineering components in food-processing equipment. SCOPIC® technology can provide metal and X-ray detectability while formulations can be optimised for the mechanical, processing and colour requirements of the finished component.
Detectable PA6 and other nylon formulations are available for injection-moulded and extruded engineering components. Formulations can be tailored to balance detectability with properties including toughness, stiffness, wear resistance and processability.
Polyketone offers an attractive combination of toughness, wear resistance, chemical resistance and low moisture absorption for demanding engineering applications. SCOPIC® detectable polyketone compounds can be developed in a range of colours, including unusually light and bright formulations, for components used in food-processing environments.
SCOPIC® technology can also be incorporated into PP and PE for applications requiring the chemical resistance, low density or processing characteristics of polyolefins. Masterbatch and fully compounded solutions can be tailored to the required level of metal and/or X-ray detectability.
Detectable materials are not limited to rigid plastic components. Seals, gaskets, flexible connectors and other elastomeric parts can wear, tear or shear during use, potentially creating polymer fragments that are difficult to identify with conventional inspection systems.
Radical Materials develops metal and X-ray detectable masterbatches and compounds for silicone, NBR, SBR, natural rubber and other elastomer systems. Masterbatches can be formulated using generic or customer-specified base elastomers, allowing existing material systems to be retained where appropriate.
Our in-house mixing capability also allows complete detectable elastomer compounds to be developed where a ready-to-process material is preferred.
Detectability can additionally be combined with other properties, including antimicrobial, electrically conductive or thermally conductive functionality, within the same formulation.
Metal detection, X-ray detection and visual detection identify contamination in different ways, and each has its own strengths and limitations. Performance depends on factors including fragment size, material composition, product type, packaging and the detection equipment being used.
SCOPIC® formulations can be optimised for metal detection, X-ray detection or both, while contrasting colours can provide an additional level of visual identification.
| | Metal detection | X-ray detection | Visual detection |
|---|---|---|---|
| What generates detection? | Electromagnetic response | X-ray attenuation/contrast | Colour contrast |
| Standard plastics | Generally not detectable | Often difficult | Depends on colour |
| SCOPIC modification | Specific detectable additive system | X-ray-optimised additive system | Bright/contrasting colour |
| Main variables | Fragment size/orientation, aperture, product effect, detector settings | Thickness, composition, product depth, food type, packaging, detector settings | Colour/background/visibility |
A single SCOPIC® formulation can provide metal, X-ray and visual detectability where specifically formulated and tested for all three requirements.
Conventional unfilled plastics do not normally produce a sufficient response in industrial metal detection systems. Metal detectable plastics contain additives that interact with the electromagnetic field generated by the detector, allowing fragments of the polymer to produce a measurable signal.
A typical balanced-coil metal detector uses a transmitter coil and receiver coils to generate and monitor an electromagnetic field. When a sufficiently detectable material passes through the aperture, it disturbs the balance of that field, producing a signal that can trigger an alarm or automatic rejection system.
Detection sensitivity depends on the formulation, fragment size and orientation, detector aperture, product effect, line speed and machine settings. The performance of a detectable polymer should therefore be confirmed under conditions representative of the final application.
Industrial X-ray inspection systems identify foreign bodies by measuring differences in X-ray attenuation as radiation passes through the product. The amount of X-ray energy absorbed depends on factors including the material’s composition, density and thickness.
Conventional polymers generally consist of relatively low atomic-number elements and often have attenuation characteristics similar to food products. As a result, small fragments of unfilled PE, PP, TPU and many other plastics can be extremely difficult for an X-ray system to distinguish from the surrounding product.
X-ray detectable plastics contain specially selected additives that increase X-ray attenuation and therefore create greater contrast between the polymer fragment and the food product.
Detection performance is application-specific. Important factors include fragment size and thickness, polymer formulation, food composition and consistency, product depth, packaging, orientation and the settings and capabilities of the X-ray inspection system.
For this reason, X-ray detectability should be evaluated using representative materials and conditions rather than inferred simply from the density of the compound.
Radical Materials uses industrial metal detection and Minebea X-ray inspection equipment within our development laboratory to measure and compare the detection performance of SCOPIC® formulations.
Testing allows us to evaluate representative fragment sizes, compare additive systems and optimise formulations for the required detection method. Where appropriate, samples can also be assessed against representative food products or application conditions.
Detectability is highly dependent on the detector, product, fragment geometry and operating conditions, so our objective is to generate meaningful comparative data rather than rely on generic claims that a material is simply “detectable”.
Metal and X-ray detectable polymers are widely used in and around food-processing equipment, including components intended for direct, indirect or incidental food contact.
Food-contact suitability depends on the complete material formulation, finished article, conditions of use and market in which the product will be placed. For this reason, regulatory compliance cannot be determined solely from the status of the detectable additive or masterbatch.
Radical Materials supports relevant SCOPIC® formulations with regulatory declarations, composition information and migration testing where appropriate, helping customers complete the assessment required for their finished component.
Plastic food-contact materials placed on the market in Great Britain are subject to the applicable GB food-contact framework, including the assimilated requirements derived from Regulation (EC) No 1935/2004 and Regulation (EU) No 10/2011.
Relevant SCOPIC® additives and masterbatches have been evaluated using migration testing at concentrations at or above typical recommended use levels. Where applicable, supporting declarations specify the materials tested, migration conditions, limitations and intended conditions of use.
These documents are available to customers to support assessment of the finished food-contact article.
For products intended for the European Union, relevant SCOPIC® formulations can be supported with information relating to Regulation (EC) No 1935/2004 and the applicable requirements of Commission Regulation (EU) No 10/2011, including migration data where available.
Compliance must ultimately be assessed against the intended polymer, additive concentration, food type, contact time, temperature and other conditions applicable to the finished article.
Relevant SCOPIC® detectable additive systems have been subjected to migration testing under defined conditions to support assessment for US food-contact applications.
The resulting data can be used alongside the applicable FDA regulatory status of the individual substances and intended conditions of use when assessing the finished article. Where relevant, testing can also provide supporting information for assessment against the principles and thresholds described under 21 CFR 170.39.
Full test conditions, results and supporting statements are available on request.
Depending on the SCOPIC® product and intended application, supporting documentation can include food-contact declarations, substance information, migration test results and defined conditions or limitations of use.
Customers should use this information as part of the regulatory assessment of the complete finished article. Our technical team can provide the relevant documentation and discuss application-specific requirements during material selection and development.
A range of masterbatches and additives which are compatible with a wide range of polymers and offer a simple and effective way of adding levels of metal detectable and/or X-ray detectable properties to products.
Masterbatch and compound can be developed to suit specific requirements and applications.
A large proportion of our work is the development of custom solutions, often outside the scope of our standard product range. We relish a challenge, so feel free to test our capabilities.
Detectability requirements vary with the polymer, component geometry, inspection system and intended application. We develop formulations around the complete performance requirement, balancing metal and/or X-ray detectability with mechanical properties, processing, colour and regulatory considerations.
Small development batches can be compounded in-house for processing trials and initial evaluation. Where required, materials can be moulded or otherwise converted into representative specimens to assess detectability and material performance before scale-up.
Formulations can be evaluated using in-house metal and X-ray inspection equipment alongside mechanical and application-specific testing. This allows additive level, polymer formulation and finished-component performance to be optimised together.
Once a formulation has been validated, it can be progressed from development quantities into routine commercial production. Standard and custom SCOPIC® masterbatches and compounds are manufactured in-house, providing continuity from initial formulation through to ongoing supply.
Answers to common questions about metal and X-ray detectable plastics, masterbatches and compounds, including how detectable materials work, what affects detection performance, compatible polymers, food-contact considerations and how SCOPIC® formulations can be tailored to specific applications.
If you can’t find the answers you need, please don’t hesitate to contact us.
Not necessarily. Metal detection and X-ray inspection operate using different physical principles, so a material optimised for metal detection will not automatically provide good X-ray visibility.
Some detectable additives improve performance with both systems, but where reliable dual detection is required, the formulation should be developed and tested specifically for both metal and X-ray detectability.
There is no single detection value that applies to every application. Detectability depends on the polymer formulation, additive concentration, fragment size and shape, inspection equipment, operating settings and the product being inspected.
Radical Materials uses in-house metal detection and X-ray inspection equipment to compare formulations and optimise SCOPIC® materials under controlled conditions. Final detection performance should always be validated using equipment and operating conditions representative of the intended application.
The smallest detectable fragment depends on much more than the detectable material itself. Important factors include additive loading, polymer type, fragment thickness and orientation, detector aperture, line speed, product effect, food composition, packaging and equipment sensitivity.
For X-ray systems, product depth and the difference in X-ray attenuation between the fragment and surrounding product are particularly important. For this reason, claims of a universal minimum detectable fragment size should be treated with caution.
It can. Detectable additives are typically inorganic materials and, at sufficiently high loading levels, may affect properties such as impact strength, elongation, flexibility, density and processing behaviour.
The objective is therefore not simply to maximise additive loading. SCOPIC® formulations are developed to achieve the required detectability while minimising unwanted effects on the base polymer. Where necessary, impact modifiers, processing aids or other formulation changes can be used to help maintain finished-component performance.
Detectable functionality can be incorporated into a wide range of thermoplastics and elastomers, including polypropylene (PP), polyethylene (PE), TPU, nylon/polyamide (PA), POM/acetal and polyketone (PK/POK).
Solutions can also be developed for silicone, natural rubber, NBR, SBR and other elastomers. The optimum detectable system depends on the polymer, processing conditions, required detection performance and finished application.
Yes. Metal and X-ray detectable technologies can be incorporated into silicone and a range of natural and synthetic rubbers.
Typical applications include seals, gaskets, flexible connectors, bellows and other elastomeric components used around food and pharmaceutical processing equipment. Formulations can be supplied as masterbatches or, where appropriate, as complete ready-to-process compounds.
Yes, detectable materials can be formulated for food-contact applications, but compliance must be assessed for the complete formulation, finished article, intended conditions of use and target market.
The regulatory status of the detectable additive alone does not automatically establish compliance of the finished component. Radical Materials can provide relevant regulatory declarations and supporting migration information for appropriate SCOPIC® formulations.
Yes. Blue is widely used in food-processing environments because it provides strong visual contrast with many food products, but detectable plastics can be produced in a wide range of colours.
Colour development must take account of the base polymer and detectable filler because some high-loading detectable systems can naturally darken or mute a compound. Radical Materials can formulate bright colours and, in selected polymers, unusually light or white detectable materials while maintaining detection performance.
Yes. Metal and X-ray detectability can be combined with antimicrobial functionality and other material properties within the same compound or masterbatch system.
This can be particularly useful in food-processing components where both foreign-body control and inhibition of microbial growth are desirable. Multifunctional formulations need to be developed carefully because individual additives can interact and may influence processing, colour and mechanical properties.
There is no universal addition rate. The required concentration depends on the masterbatch formulation, polymer, required level of metal and/or X-ray detectability, component thickness, mechanical requirements and inspection equipment.
Increasing the addition rate may improve detectability, but it can also increase cost, density and the effect on mechanical properties. Radical Materials therefore aims to establish the lowest practical addition rate that achieves the required detection performance for the intended application.